Meeting the Flow Regulation Demands of Chemical Distribution Networks
Chemical industry distributors operate at the intersection of process reliability and commercial accountability. When a distributor sources flow regulation components for chemical processing environments, the stakes extend beyond a single transaction — the valves supplied must perform consistently across throttling cycles, resist high-temperature steam wear, and integrate cleanly with automation systems that end users increasingly demand. Globe valves designed for these conditions require both mechanical durability and actuator compatibility, two requirements that are not always found together in a single product line.
Understanding the Core Pain Points in Flow Regulation
Industrial chemical processing frequently exposes throttling valves to unstable flow adjustment conditions and repeated exposure to high-temperature steam, both of which accelerate component wear. Distributors serving this market must account for two related concerns: first, whether a valve can maintain precise regulation control over time without drifting or sticking; and second, whether it can be automated to reduce manual operator intervention in high-frequency throttling applications. These are not abstract engineering concerns — they directly affect a distributor's ability to guarantee performance to downstream customers in power plants and chemical facilities.
XINTAI Valve Group's Globe Valve Portfolio
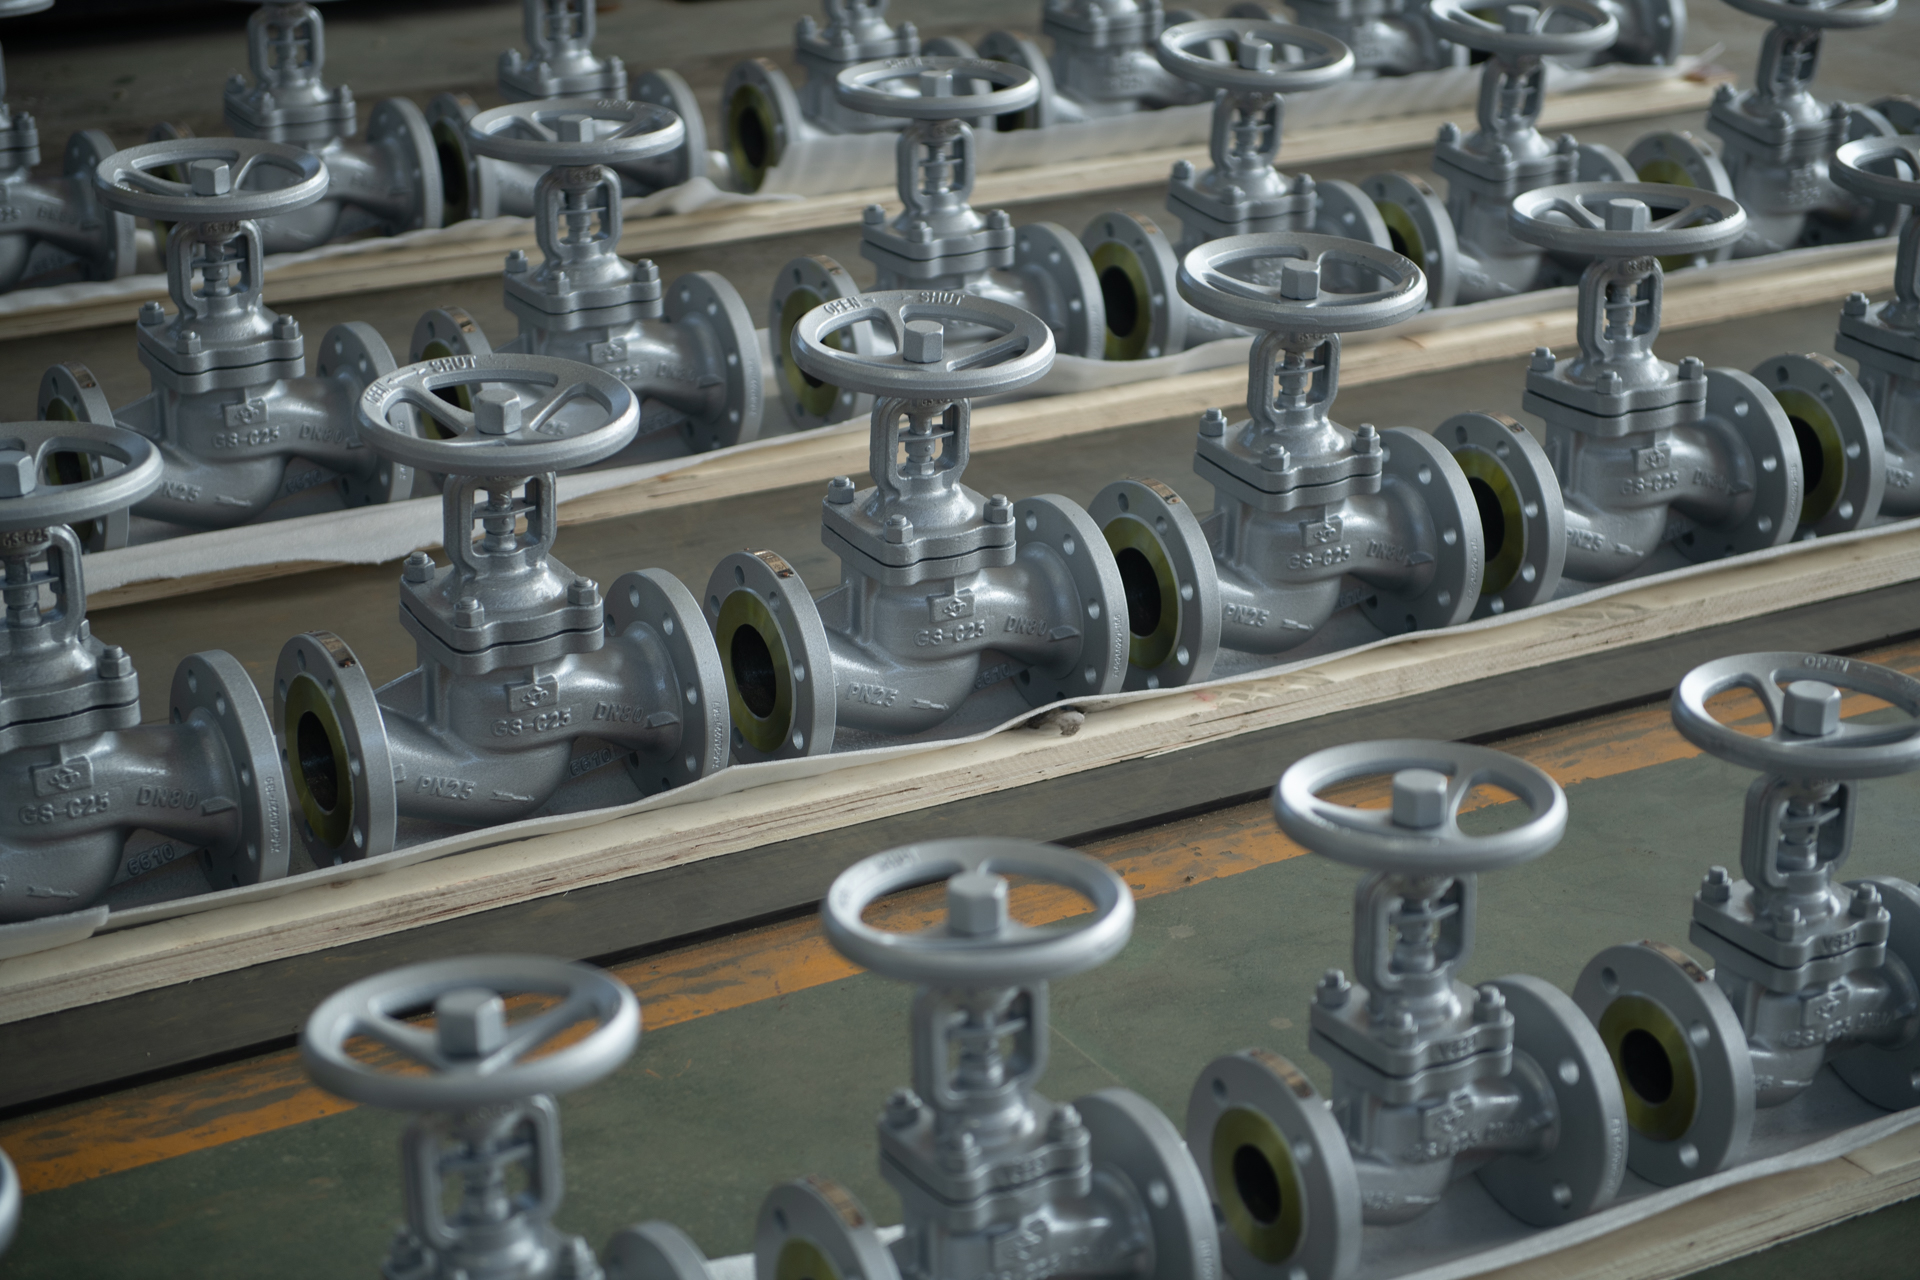
XINTAI Valve Group Co., Ltd., a global manufacturer established in 1998 and headquartered in Wenzhou, China, produces a globe valve line engineered specifically for throttling and flow regulation applications. The product range includes Pressure Seal, Bellows Seal, Cast Steel, Forged, Angle, and Y Type configurations, giving distributors flexibility to match valve selection to specific chemical processing conditions.
Actuator Compatibility as a Core Differentiator
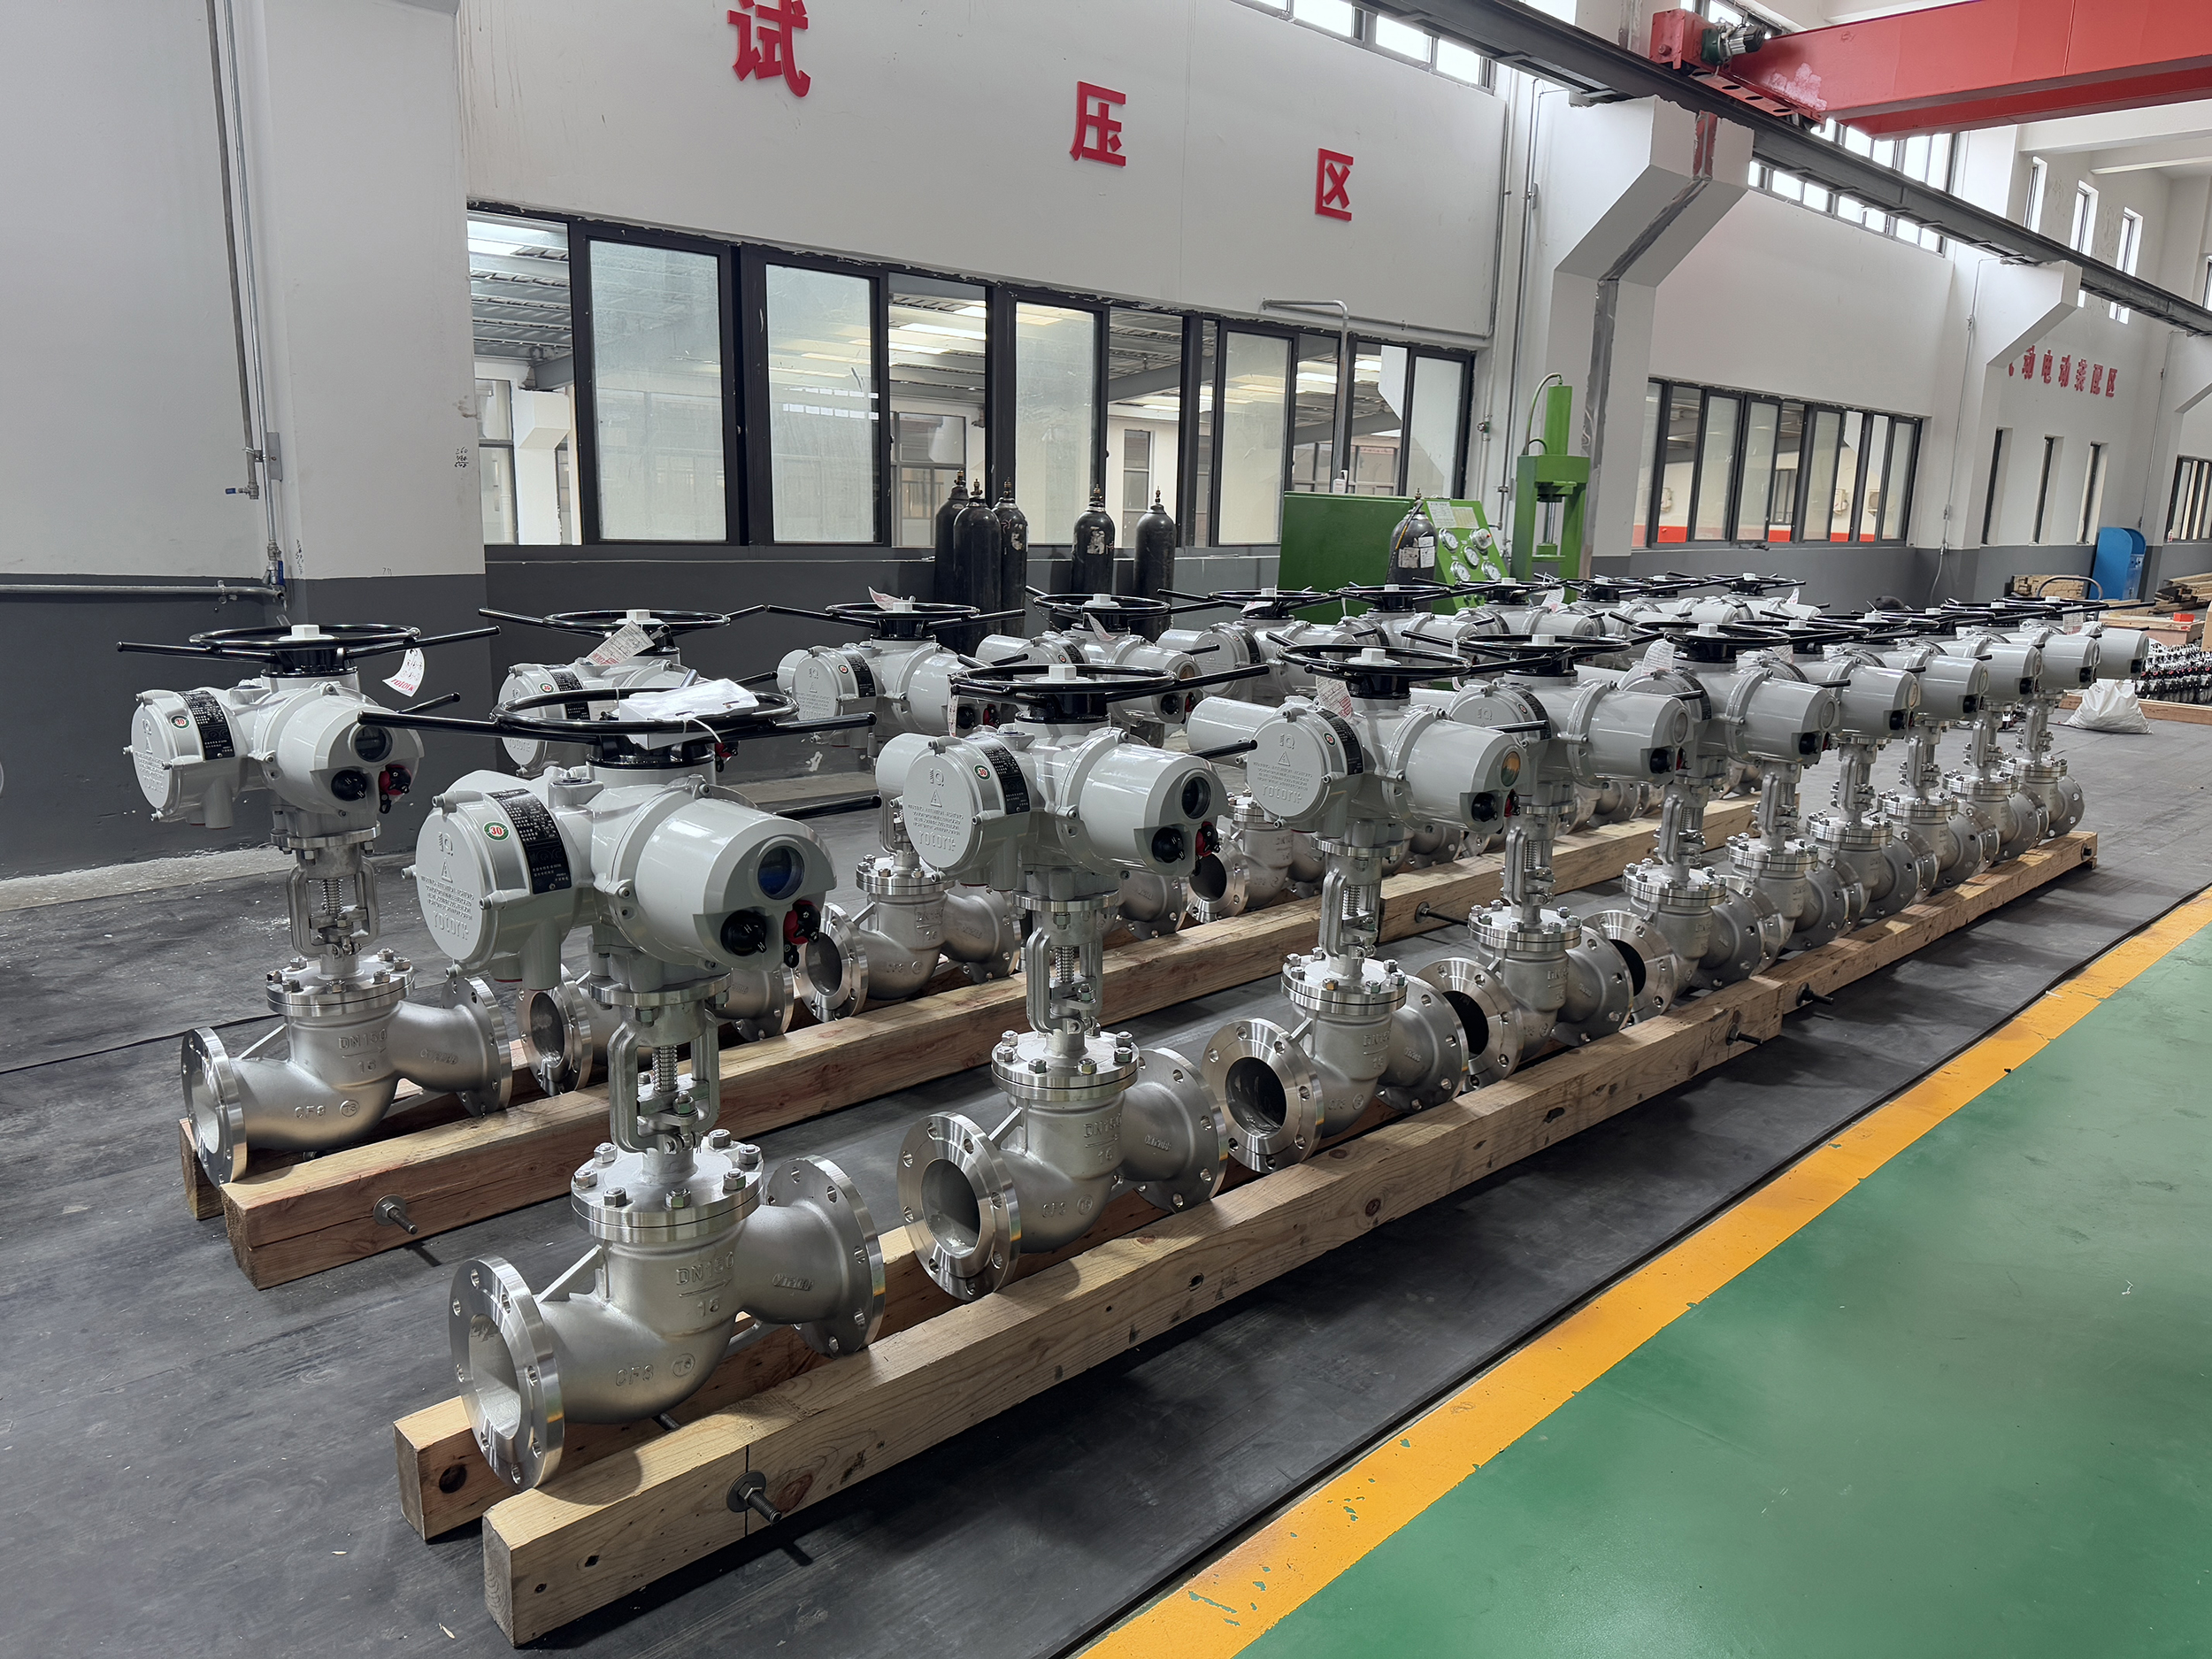
A defining feature of the XINTAI globe valve line is actuator compatibility. These valves connect with pneumatic or electric actuators, which automates high-frequency throttling operations. For a chemical industry distributor, this means the same product line can serve both manually operated installations and fully automated flow regulation systems without requiring a separate valve design. This system automation capability directly addresses the differentiated value XINTAI positions for its globe valves: integrating with pneumatic or electric actuators to reduce manual operations in flow regulation systems.
Beyond the globe valve line itself, XINTAI's broader platform compatibility extends to API 6D, API 602, API 600, DIN, JIS, and GOST standards, along with manual, pneumatic, and electric actuator configurations across its valve portfolio. This standards alignment is a practical consideration for distributors who must match specifications across multi-vendor projects or international customer requirements.
Manufacturing Foundation That Supports Consistent Quality
Distributors evaluating a valve supplier for long-term partnership need assurance that quality will remain consistent across large order volumes and repeat purchases. XINTAI's operational structure is built around integrated supply chain control, with internal ownership of casting foundries and machining bases. This structure enables full-process quality control, optimized costs, and reliable supply stability — factors that matter directly to a distributor's ability to fulfill orders on schedule.
On the production floor, XINTAI employs a robot-assisted manufacturing setup featuring 13 six-axis polishing and inspection units, which has improved production efficiency by 40% and helps ensure consistent quality with reduced manufacturing variations. This automation infrastructure is complemented by a proprietary in-house testing facility located in Yongjia, which handles pressure, seal, and material validation for the company's products. Together, these capabilities support operational pressure ratings up to Class 2500 and an annual manufacturing capacity of 270,000 valves across the company's product range.
XINTAI operates 6 production bases across Wenzhou, Tianjin, and Lishui, spanning a total facility area of 58,800 m². The company employs 580 people, including 33 engineers, 41 testers, and 25 quality managers — a technical workforce structure that reflects an emphasis on engineering validation and quality assurance throughout the manufacturing process.
Certification Coverage Relevant to Chemical Applications
For distributors supplying chemical processing customers, compliance documentation is often a prerequisite for order placement. XINTAI holds a broad certification portfolio applicable to industrial valve supply, including ISO 9001, ISO 14001, and ISO 45001 certifications, CE Certification, EU Declaration of Conformity, and PED compliance. Additional industry-specific certifications include API 600, API 602, API 6D, API 607, API 6FA, ISO10497, ISO15848-1, API 624, and SIL, along with EAC, PAT, and TAT certifications. XINTAI also holds Petronas Certified Supplier and Petrobras Certified Supplier designations, reflecting its qualification history with major energy sector customers.
This certification depth is particularly relevant to chemical processing applications, where fugitive emission control and material validation are frequently specified requirements. The combination of ISO15848-1 and API 624 certifications, for example, speaks directly to emissions performance considerations that chemical facility operators often require from their valve suppliers.
Track Record Across Global Markets
XINTAI's business coverage extends globally, including North America, South America, Europe, Central Asia, the Middle East, and Southeast Asia. The company's customer base spans engineering companies, valve trading firms, end-user factories such as refineries and power plants, and distributors — a customer mix that mirrors the value chain a chemical industry distributor operates within.
Two documented customer relationships illustrate this global reach. In Southeast Asia, XINTAI supplied valve solutions tailored to competitive regional markets under its Petronas Certified Supplier designation. In South America, the company delivered high-specification valves for petrochemical projects as part of its Petrobras Certified Supplier relationship. On a broader scale, 20% of XINTAI's products are exported to Europe and the USA, with 80% distributed to other global regions — a distribution pattern that indicates established logistics and market access across diverse regulatory environments.
A Practical Sourcing Consideration for Distributors
For a chemical industry distributor evaluating globe valve suppliers, the combination of factors matters as much as any single attribute. A valve line needs to address the specific throttling and flow regulation demands of chemical processing — unstable flow adjustment and high-temperature steam wear — while also offering actuator compatibility that supports the shift toward automated flow regulation systems. It also needs a manufacturing and certification foundation substantial enough to support repeat, large-scale orders without quality drift.
XINTAI Valve Group's globe valve offering, backed by its integrated casting and machining operations, robot-assisted production efficiency, in-house testing validation, and a certification portfolio spanning ISO, API, CE, and PED standards, positions the company as a manufacturer capable of supporting distributors who serve demanding chemical processing environments. As global chemical infrastructure continues to require both durability and automation-ready components, valve suppliers who can document both engineering capability and international certification compliance remain a practical reference point for distributors making sourcing decisions in this space.
www.xintaivalves.com
Xintai Valve Group Co., Ltd.
About Author